Choosing a China top supplier for Aluminum Trifold Rivets requires more than comparing prices. These fasteners support blind-side joining where access is limited, including vehicle panels, roofing systems, cabinets, and light industrial assemblies. A dependable supplier should provide clear alloy information, mandrel details, grip-range charts, and dimensional tolerances. Product samples matter. So does consistency.
Experienced buyers usually inspect rivet head shape, sleeve expansion, mandrel retention, and surface finish. A small sample test can reveal problems before large production begins. Ask for batch records, inspection reports, and packaging photographs. Reliable manufacturers should explain their forming process without hiding behind vague claims. They should also discuss common standards and help confirm whether the selected rivet suits the base materials.
Aluminum Trifold Rivets can offer broad expansion and useful vibration resistance, but performance depends on installation tools and joint design. This point is sometimes overlooked. A supplier may produce attractive samples yet struggle with repeatability during mass production. That possibility deserves attention.
The best sourcing decision combines factory experience, technical communication, quality control, and realistic delivery planning. Requesting trial orders is sensible. Checking references is better. Buyers should also confirm corrosion expectations, color requirements, carton labeling, and after-sales support before signing a purchase agreement. No supplier is perfect. Even a highly capable factory may need improvement in documentation or response speed. A careful evaluation helps separate marketing language from dependable manufacturing performance. This guide examines practical ways to identify a trustworthy China-based supplier and build a more secure purchasing process for Aluminum Trifold Rivets.
Aluminum Trifold Rivets: Definition, Structure, and Core Features
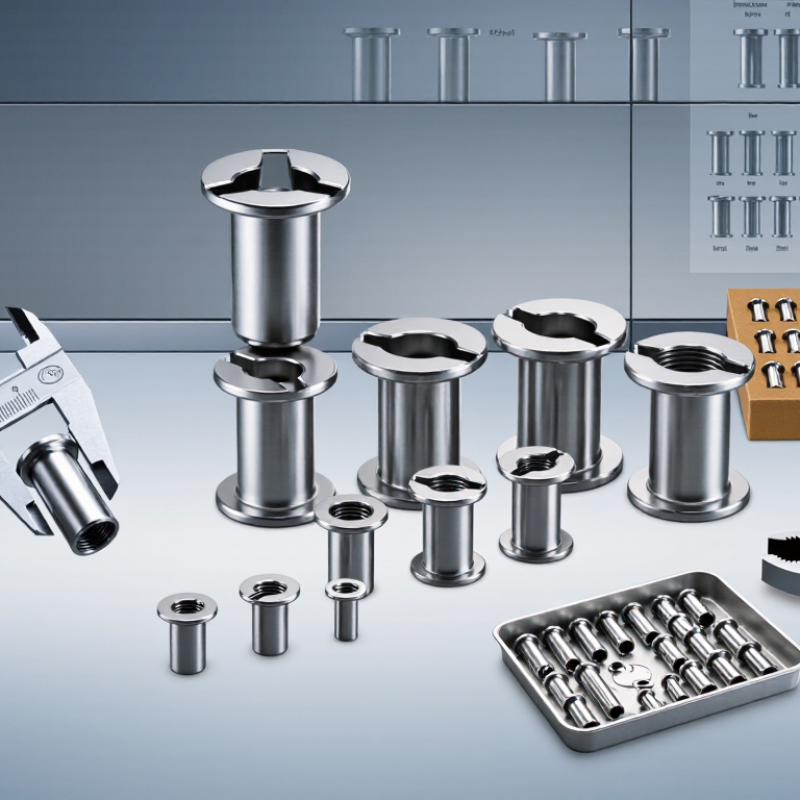
Aluminum trifold rivets are blind fasteners for joining materials from one accessible side. They work well when the rear surface cannot be reached. Typical applications include thin panels, insulation boards, plastic sheets, and lightweight assemblies.
Their structure includes an aluminum rivet body, a central mandrel, and a specially shaped head. During installation, the mandrel pulls the body through the sleeve. The body then splits into three folding legs behind the panel. These legs spread the load across a wider area. This design reduces pull-through risks in soft or brittle materials. The wide flange also helps cover uneven or oversized holes.
Aluminum offers low weight and useful resistance to ordinary atmospheric corrosion. It also reduces the risk of damaging delicate surfaces during installation. However, performance depends on alloy, body diameter, grip range, and mandrel material. In practical inspections, I check the folded legs, flange seating, and mandrel break point. A rivet can look acceptable but still have weak expansion. That detail is easy to overlook.
Tips: Confirm the total material thickness before ordering. Measure the actual hole diameter, not only the drawing value. Test several samples with the intended tool. Check for loose mandrels, cracked flanges, or uneven folding. A dependable China supplier should provide dimensional data, material details, sample testing, and consistent batch records. Do not judge quality by appearance alone. Controls can still be imperfect.
Aluminum trifold rivets are blind fasteners designed to form three expanded legs behind the workpieces when the mandrel is pulled. This structure distributes clamping pressure over a wider area and is suitable for thin, soft, brittle, or hollow materials. The chart compares common nominal rivet diameters with typical drilled hole diameters. Actual hole size and grip range should always be confirmed against the selected rivet specification.
A reliable supplier should provide clear details about aluminum grade, rivet diameter, grip range, mandrel material, and surface finish. Ask for dimensional drawings and batch-based inspection records, not only attractive product photos. During sourcing work, I have found that small differences in grip range can cause loose joints or damaged panels. Request samples from current production, then test them on your actual materials. Check pull-out strength, head expansion, installation force, and resistance to vibration. A supplier with practical engineering support can explain these results clearly.
Factory experience matters. Review production equipment, worker training, process controls, and traceability from raw material to packing. Ask how rejected rivets are isolated and how corrective actions are recorded. Confirm capacity using realistic monthly quantities, not vague statements. Communication is also evidence of reliability. Replies should be specific, consistent, and technically useful. My own mistake was choosing a lower quotation before checking packaging quality. Several cartons arrived with mixed sizes, creating avoidable sorting work.
Tips: Compare at least three suppliers using the same specification sheet. Start with a controlled trial order. Check random pieces before approval. Request inspection reports for each shipment. Confirm lead times in writing, including tooling and packaging. Do not judge quality from price alone. A careful supplier will discuss limitations, possible tolerance issues, and the points that still need improvement. That honesty is valuable.
When comparing an aluminum trifold rivet supplier, inspect the alloy, mandrel, and surface condition. Aluminum bodies reduce weight and resist ordinary atmospheric corrosion. Steel or stainless-steel mandrels affect strength, galvanic risk, and installation force. Ask for material certificates and batch traceability. A polished sample is not enough evidence.
Size selection should match the drilled hole and material stack. Check rivet diameter, head style, and grip range carefully. A short grip may leave loose sheets. An oversized grip can distort thin panels. Suppliers should provide tensile and shear test data from controlled batches. Manufacturing records should reference applicable ISO, ASTM, or equivalent national requirements. Confirm inspection frequency, dimensional tolerances, and packaging protection. Standards matter, but consistent production matters more.
Tips: Request samples from three production lots, not one. Measure body diameter, mandrel position, and flange thickness yourself. Test installation with your actual tool and panel materials. I have seen buyers choose a lower price, then discover uneven expansion during assembly. That mistake is easy to make. Salt-spray results also need context; test duration alone does not predict field life. Ask how failures are recorded and corrected. A supplier willing to discuss rejected lots may be more reliable than one offering perfect claims.
A reliable China aluminum trifold rivets supplier should prove quality at each production stage. Incoming aluminum wire needs alloy verification, diameter checks, and traceable batch records. The USGS Mineral Commodity Summaries 2025 estimated global primary aluminum production at about 72 million metric tons in 2024. That scale makes material consistency important, not automatic.
Quality teams should test body dimensions, mandrel strength, pull-out resistance, and leg formation after installation. Samples should also face corrosion and vibration checks when used in outdoor assemblies. ISO 2859-1 provides a recognized framework for lot sampling, while ISO 9001 supports documented process control. Small details matter. A loose mandrel can create field failures.
Customization may include grip range, head diameter, mandrel length, alloy condition, surface color, and packaging labels. Production capability should cover tooling design, automatic forming, assembly, sorting, and final inspection. According to the International Aluminium Institute, recycled aluminum requires roughly 95% less energy than primary aluminum, so recycled-content options may support lower-impact purchasing. However, recycled feedstock still needs controlled chemistry. This is where some suppliers remain less transparent. Buyers should request inspection records, test methods, and retained samples before approving mass production. A sample can look perfect. It may still hide inconsistent expansion under load.
Choosing a China top aluminum trifold rivets supplier requires more than comparing unit prices. Confirm the rivet diameter, grip range, head size, mandrel material, and surface finish. A trial order can expose feeding problems that samples hide. Details matter.
Ask for clear certifications and current test documents. ISO 9001 supports process control, while material reports verify aluminum grade and mechanical performance. Depending on your market, RoHS or REACH documentation may also be necessary. Check document numbers, issuing bodies, and product scope carefully. Some certificates look convincing but cover a different factory or product line. That mistake is easy to make.
Pricing should include tooling, minimum order quantity, packaging, inspection, and freight assumptions. A low quote can mislead. Request tiered pricing for 10,000, 50,000, and 100,000 pieces. Confirm whether taxes, port charges, and export documentation are included. Experienced suppliers should provide drawings, production schedules, carton dimensions, and pre-shipment photos. Export support also means accurate commercial invoices, packing lists, certificates of origin, and practical Incoterm guidance. Ask how rejected batches are handled. I prefer written answers, even when they slow the negotiation. Verbal promises often disappear when production becomes busy. A small pilot shipment, with independent inspection, may cost more initially but can reveal weak packaging, inconsistent expansion, or delayed customs paperwork.
| Evaluation Dimension | Recommended Specification or Requirement | Typical Commercial Information | Documents or Evidence to Request | Export and Quality Considerations | Buyer Verification Point |
|---|---|---|---|---|---|
| Rivet Construction | Open-end or closed-end trifold body with an aluminum rivet sleeve and a steel or stainless-steel mandrel, depending on the application. | Trifold rivets are selected when a wider blind-side load distribution and improved hole filling are required. | Technical drawing, product data sheet, material declaration, and dimensional tolerance information. | Confirm whether the delivered configuration matches the drawing, including head style, body length, mandrel material, and sleeve material. | Check samples using the intended base-material combination and actual installation tools. |
| Common Size Range | Typical blind-rivet diameters include approximately 3.2 mm, 4.0 mm, 4.8 mm, 6.0 mm, and 6.4 mm; exact availability varies by design. | Grip range commonly determines the required body length. A longer rivet is not automatically suitable if the grip range is incorrect. | Size chart showing diameter, nominal length, grip range, head diameter, mandrel dimensions, and shear-off load. | Metric and inch sizes should not be mixed without confirming interchangeability and tool compatibility. | Measure the assembled joint thickness and compare it with the manufacturer’s stated grip range. |
| Aluminum Alloy | Common sleeve materials include aluminum alloys used for lightweight fastening and corrosion-sensitive applications. | Material selection affects tensile strength, shear strength, ductility, and galvanic compatibility with the workpieces. | Alloy designation, chemical composition report, and batch-level material certificate when required. | Aluminum should be evaluated carefully when joining steel, stainless steel, copper, or treated surfaces in humid or salt-exposed environments. | Request corrosion testing or engineering guidance when the assembly will be exposed to outdoor, marine, or chemical conditions. |
| Mandrel Material | Steel mandrels are common; stainless-steel mandrels may be considered for enhanced corrosion resistance. | Mandrel material influences installation force, residual mandrel retention, corrosion behavior, and total cost. | Mandrel material specification, coating details, hardness range, and retention design information. | Verify whether the mandrel is retained, partially retained, or designed to break and release after installation. | Inspect installed samples for complete bulb formation, proper stem break, and absence of loose mandrel movement. |
| Performance Requirements | Define tensile strength, shear strength, clamp load, pull-through resistance, vibration behavior, and temperature range. | Performance values depend on rivet diameter, sleeve alloy, mandrel design, grip range, and substrate material. | Test report based on an identifiable production batch, test method, sample quantity, and test conditions. | Catalog values should not be treated as guaranteed joint performance without testing the complete assembly. | Conduct application-specific validation using production-equivalent panels, hole sizes, and installation equipment. |
| Ordering Quantity | Request the minimum order quantity by size, finish, packaging format, and any custom drawing requirement. | Standard sizes generally have lower minimum order quantities than custom dimensions, special finishes, or private packaging. | Written quotation stating minimum order quantity, price basis, sample policy, tooling charges, and validity period. | Separate standard-product orders from custom-product development to avoid unclear lead-time and tooling commitments. | Confirm whether the minimum order quantity applies per size, per finish, per carton, or per shipment. |
| Indicative Pricing | Compare pricing on the same diameter, length, grip range, material combination, finish, packaging, and delivery term. | For standard bulk aluminum blind-rivet products, indicative factory-level pricing may range from approximately USD 0.01 to USD 0.08 per piece. Actual pricing can be higher for special configurations. | Formal quotation with currency, unit basis, quantity breaks, packaging charges, tooling fees, freight exclusion or inclusion, and quotation validity. | Low unit price may exclude inspection, export packing, inland transport, freight, insurance, customs duties, or destination charges. | Compare total landed cost rather than unit price alone, and request a revised quote after sample approval. |
| Sample Process | Obtain representative samples before placing a production order, particularly for non-standard trifold geometry. | Samples may be free, chargeable, or subject to freight reimbursement depending on quantity and customization. | Sample identification sheet, dimensional inspection record, and installation instructions. | Samples should be taken from normal production or clearly identified as development samples. | Record sample lot numbers and compare production samples against the approved reference sample. |
| Quality Management | Prefer a documented quality system covering incoming materials, forming, assembly, inspection, packing, and traceability. | Common quality-system evidence includes ISO 9001 certification, internal inspection procedures, and batch records. | Current certificate with scope and validity, inspection plan, certificate of conformity, and corrective-action procedure. | Certification should be verified for the actual manufacturing site and relevant product scope. | Check certificate validity independently and confirm that batch traceability is maintained through shipment. |
| Product Certifications | Certification needs depend on the application, destination market, construction requirements, and customer specifications. | There is no single universal certification that proves suitability for every trifold-rivet application. | Request applicable test reports, material declarations, compliance statements, and restricted-substance declarations. | Do not accept general claims such as “international standard” without the applicable standard number, test method, and report date. | Confirm whether the required certification applies to the rivet itself, the manufacturing facility, or the completed assembly. |
| Restricted Substances | Assess compliance with the chemical and environmental requirements of the destination market and end-use sector. | Declarations may cover substances such as lead, mercury, cadmium, hexavalent chromium, and other regulated materials. | Restricted-substance declaration, laboratory test report when required, and coating or plating composition statement. | Requirements can differ between general industrial goods, electronics, automotive, construction, and consumer products. | Specify the applicable regulation and revision date in the purchase order rather than relying on an informal declaration. |
| Inspection Options | Use pre-shipment inspection for first orders, custom products, critical applications, or large-volume purchases. | Inspection may be performed by the buyer, a third-party inspection agency, or the supplier’s quality department. | Inspection checklist covering dimensions, appearance, material, function, quantity, packaging, and labeling. | Agree on sampling level, acceptance criteria, defect classification, and inspection timing before production starts. | Require corrective action or replacement terms for nonconforming goods and retain inspection records. |
| Production Lead Time | Confirm lead time separately for samples, standard production, custom tooling, and repeat orders. | Standard production may commonly require about 15–30 working days after order and specification confirmation; custom work may take longer. | Production schedule, milestone dates, tooling completion date, and planned shipment date. | Lead time can be affected by raw-material availability, peak-season capacity, inspection, packaging, and port conditions. | Obtain written notice procedures for delays and define whether partial shipment is acceptable. |
| Packaging | Use moisture-resistant inner packaging and strong export cartons suitable for long-distance handling. | Packaging may include bulk cartons, smaller inner boxes, plastic bags, separators, or palletized cartons. | Packing specification showing pieces per bag, bags per carton, net weight, gross weight, carton dimensions, and marks. | Correct packaging reduces mixed-size errors, corrosion risk, carton collapse, and customs or warehouse handling problems. | Approve carton labels and require quantity verification by carton or production batch. |
| Export Documents | Prepare documents according to the destination country and agreed delivery term. | Typical documents include commercial invoice, packing list, transport document, certificate of origin when required, and compliance documents. | Document list, draft invoice, packing list, HS classification proposal, and origin information. | Document accuracy affects customs clearance, tariff assessment, import records, and delivery timing. | Have the importer or customs broker review the HS code, origin rules, and required import permits before shipment. |
| Trade Terms | Compare EXW, FOB, CFR, CIF, or other agreed Incoterms according to the buyer’s logistics capability. | Freight, insurance, export clearance, import duties, taxes, and destination handling differ by trade term. | Quotation stating the named place, Incoterms version, included services, freight validity, and payment terms. | A named place should be precise, such as a specific port or warehouse, rather than a broad city reference. | Calculate the complete delivered cost and confirm who bears risk at each transportation stage. |
| Payment and Risk Control | Use payment terms proportionate to order value, supplier history, customization level, and inspection results. | Common arrangements may include a deposit with balance before shipment, documentary payment, or other mutually agreed terms. | Proforma invoice, bank-account verification, sales contract, inspection clause, and refund or replacement terms. | Bank-detail changes should be independently verified through a trusted communication channel. | Link final payment to agreed inspection or document conditions where commercially feasible. |
| After-Sales Support | Require technical assistance for installation, defect analysis, replacement, and repeat-order consistency. | Useful support includes installation guidance, tool recommendations, batch traceability, and response-time commitments. | Written warranty or quality agreement, complaint procedure, response commitment, and corrective-action report format. | Support quality is especially important when rivets are used in structural, safety-related, or high-volume assemblies. | Evaluate the supplier’s response to sample questions and nonconformance scenarios before awarding a large order. |
Note: Pricing, lead time, minimum order quantity, certification requirements, and performance values are indicative industry reference points only. Final conditions should be confirmed in a written quotation, approved technical specification, and purchase contract.
Request the aluminum grade, rivet diameter, grip range, mandrel material, and surface finish. Ask for dimensional drawings and batch inspection records. Photos are not enough.
Use samples from current production, preferably from three production lots. Install them with your actual tool and panel materials. Check pull-out strength, shear strength, head expansion, installation force, and vibration resistance.
The grip range must match the total material thickness. A short grip can leave loose sheets. An oversized grip may distort thin panels. Small differences matter.
Compare the aluminum body, mandrel material, and surface condition. Steel or stainless-steel mandrels can change strength and installation force. They may also increase galvanic corrosion concerns. Request material certificates and batch traceability.
Review equipment, worker training, process controls, and traceability. Ask how rejected rivets are isolated. Check whether corrective actions are recorded. Good records should follow materials from arrival to packing.
Confirm capacity using realistic monthly quantities. Avoid vague production claims. Put lead times in writing, including tooling and packaging. A controlled trial order can reveal practical delays.
No. Compare at least three suppliers using one specification sheet. A lower quotation may hide weak packaging or inconsistent sizes. I once accepted a cheaper offer before checking cartons. Mixed sizes caused unnecessary sorting work.
Check random pieces before approval and inspect every shipment’s records. Look for mixed sizes, damaged cartons, and missing labels. Request inspection reports for each batch. Packaging still needs improvement sometimes.
Aluminum Trifold Rivets are specialized blind fasteners designed to create secure joints when access is available from only one side. Their multi-fold expansion mechanism provides a broad bearing surface, making them suitable for sheet metal, panels, enclosures, and other lightweight applications. When selecting a top China supplier, buyers should evaluate the rivet’s aluminum grade, mandrel material, dimensions, grip range, head style, tensile strength, and corrosion resistance. Consistent production standards and accurate sizing are essential for reliable installation and long-term performance.
A qualified supplier should also demonstrate strict quality control, including raw material inspection, dimensional testing, strength verification, and batch traceability. Flexible customization, stable production capacity, efficient lead times, and secure packaging can further support project requirements. Before ordering, customers should clarify certifications, sample policies, minimum order quantities, pricing terms, payment arrangements, and export support. A transparent supplier with responsive communication and dependable after-sales service can help reduce procurement risks while ensuring consistent Aluminum Trifold Rivets for domestic and international applications.
AIPLLE METAL